Search News
Industry Portal
Hot Articles
- Mark-and-Verify Solutions for Food Packaging: Choosing Codes, Labels, and ChecksMark and verify solutions for food packaging: choose reliable codes, durable labels, and automated checks to protect traceability, compliance, and brand trust.
- PPCS Compliance Explained: Packaging Data, Documentation, and Audit ControlsPPCS compliance explained: build traceable packaging data, controlled documentation, and audit-ready controls to reduce risk and strengthen market confidence.
- PPWD Compliance: How Packaging Producers Can Prepare for EU Waste RulesPPWD compliance guide for packaging producers: prepare for EU waste rules with smarter materials, recyclability, EPR planning, and practical design steps.
Popular Tags
PPCS Compliance Explained: Packaging Data, Documentation, and Audit Controls
Time
Click Count
Packaging compliance rarely fails because a team has no test report. It fails because the report cannot be connected—quickly and convincingly—to the exact material, supplier lot, artwork revision, market, and product it was meant to support. A film specification sits in one folder, a migration declaration in another, and a thermal ribbon qualification in an email thread that disappeared after a supplier change. When an auditor, regulator, customer, or internal safety team asks a simple question, the answer becomes difficult to prove.
PPCS compliance provides a practical way to prevent that gap. In this context, PPCS is a packaging control framework that brings together product specifications, compliance declarations, test evidence, traceability records, sustainability claims, and audit routines. For quality and safety managers, the objective is not to create more paperwork. It is to ensure that every package-facing material has a clear evidence trail from approval through use, change control, and market release.
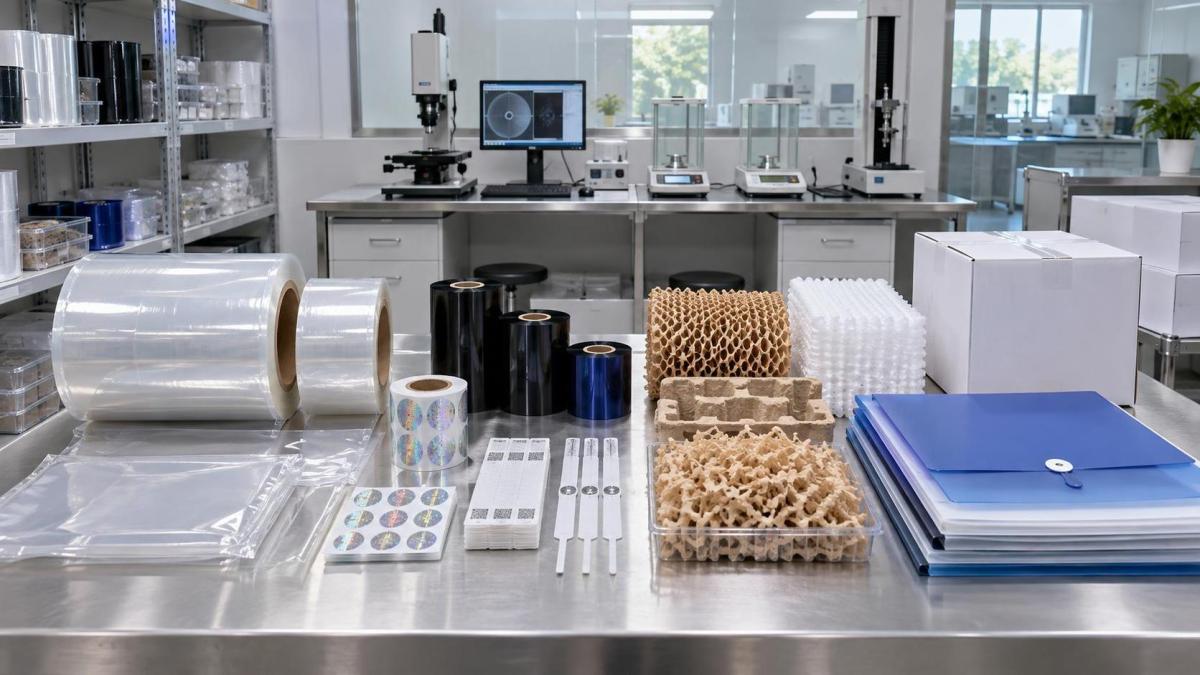
This matters across films, anti-counterfeit labels, biodegradable cushioning, thermal transfer ribbons, inks, and decorative foils. These consumables may look secondary beside the product itself, yet each can affect shelf life, readability, transport safety, tamper evidence, recycling outcomes, and customer trust.
What PPCS Compliance Should Mean in Practice
PPCS compliance should not be treated as a single certificate or a universal legal standard. Different markets, product categories, and applications remain subject to their own requirements: food-contact rules, chemical restrictions, packaging waste obligations, transport labeling rules, pharmaceutical traceability expectations, or customer-specific specifications. The value of PPCS is in organizing those obligations into a controlled, auditable operating system.
A sound PPCS program answers five questions for every approved packaging component:
- What is it? A uniquely identified material with a current technical specification.
- Where is it used? Linked to the product, packaging level, production site, and intended market.
- What requirements apply? Regulatory, safety, performance, environmental, and customer requirements are mapped rather than assumed.
- What proves conformity? Supplier declarations, test reports, certificates, artwork approvals, and inspection records are controlled as evidence.
- What happens when something changes? Material, formula, supplier, print layout, coating, or legal changes trigger documented review before release.
This approach is especially useful when procurement seeks lower-cost alternatives or operations need to switch suppliers quickly. A substitute may appear identical in width, gauge, or color, while its adhesive chemistry, recycled-content claim, migration profile, barcode durability, or end-of-life pathway differs materially.
Build the Record Around the Packaging Component, Not the Document Type
Many documentation systems are arranged by document category: all declarations in one directory, all specifications in another, all test reports elsewhere. That structure is understandable, but it creates friction during an audit. Auditors do not usually ask, “Show me your declarations.” They ask, “Show me the evidence for the label on this product shipped to this region during this period.”
A PPCS compliance file is stronger when it is built around a controlled component record. Each record should have a stable internal ID and connect the physical material to its relevant evidence. The level of detail should match risk. A plain secondary corrugated shipper needs a different evidence depth than a security label applied to a medicine carton or a high-barrier PET film protecting moisture-sensitive electronics.
At a minimum, the component record should include the material name, internal code, supplier and manufacturing site, intended use, approved specification revision, applicable markets, and approval status. It should also identify whether the material is direct food contact, indirect contact, non-contact, reusable, recyclable, compostable, security-sensitive, or safety-critical.
Data fields that prevent avoidable confusion
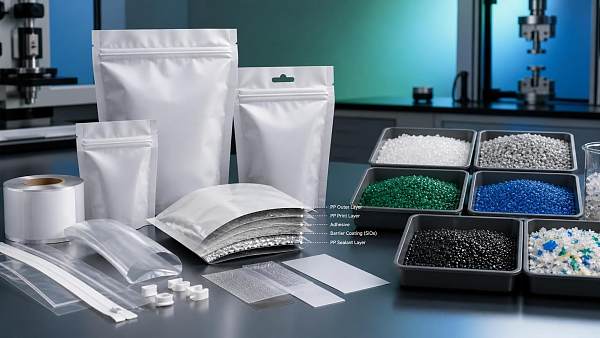
For polymer films, record resin family, structure, thickness tolerance, coating layers, barrier performance where relevant, seal conditions, and any declared recycled or bio-based content. A BOPP or PET film may be technically robust, but the compliance record must also clarify whether metallization, primers, adhesives, pigments, or barrier coatings affect recyclability or product-contact suitability.
For pressure-sensitive and anti-counterfeit labels, include facestock, adhesive type, liner, release behavior, storage limits, application temperature range, and authentication features. If a tamper-evident label leaves a “VOID” pattern after removal, that visible outcome should be part of the approved performance criteria—not simply a supplier marketing statement. Security features also need controlled artwork and access rules so that obsolete designs cannot re-enter production.
For thermal transfer ribbons and inks, document the compatible printhead and substrate, print settings, barcode symbology, legibility target, abrasion and environmental resistance requirements, and shelf-life conditions. A code that scans at the production line but fails after friction, humidity, sunlight, freezer exposure, or warehouse handling can turn a routine shipment into a traceability incident.
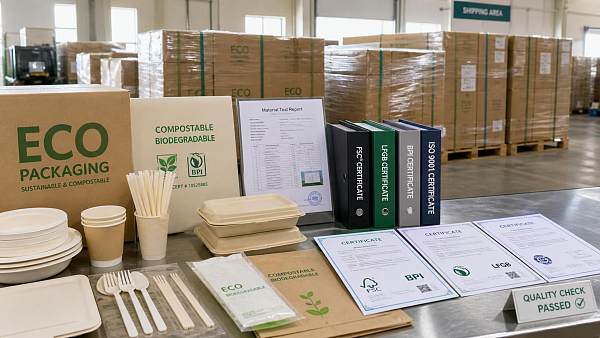
Biodegradable cushioning deserves equally disciplined treatment. Terms such as “compostable,” “biodegradable,” and “plastic-free” are often used loosely in commercial conversations. The record should state the exact material construction, declared disposal route, supporting evidence, and limitations. Industrial-composting suitability does not automatically mean a material will break down in home compost, soil, or normal recycling streams.
From Supplier Declaration to Defensible Evidence
A supplier declaration is important, but it is only one layer of evidence. Quality teams should distinguish between a statement of intent and proof that is current, applicable, and traceable to the supplied material. The more safety-critical or regulated the application, the less wise it is to rely on a generic declaration with no product code, revision date, market scope, or authorized signatory.
A useful evidence hierarchy begins with the approved technical specification and bill of materials. It then links to supplier declarations, certificates or regulatory statements where relevant, test reports, safety data, artwork proofs, incoming inspection records, and change notifications. Every file should identify the material or version it supports. If the link is indirect, record the rationale.
For example, a high-barrier film used for food or sensitive goods may require a documented review of material composition, intended contact conditions, supplier compliance statements, and test evidence appropriate to the risk. A quality manager does not need to become a polymer chemist, but should be able to ask whether a new coating, adhesive, or print layer has changed the basis of the existing assessment.
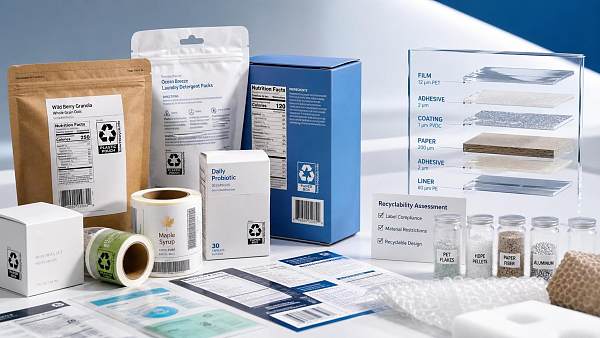
The same discipline applies to environmental claims. A recycling statement should specify the package configuration it refers to. A mono-material film may be easier to recycle than a multilayer alternative, but labels, inks, adhesive residues, metallized layers, closures, and local collection infrastructure can alter the real-world outcome. PPCS documentation should preserve these conditions rather than reducing them to a broad green claim.
Audit Controls That Work on the Factory Floor
Audit readiness is not achieved in the week before an audit. It is created through small, repeatable controls that reflect how packaging actually moves through purchasing, receiving, production, warehousing, and release.
Start with an approved-materials list that production and procurement can access easily. The list should show active status, approved supplier, version, permitted use, and any restrictions. If a material is under review or has expired evidence, its status should be unmistakable. A spreadsheet can support this at a small scale, provided ownership, revision history, and access control are maintained. Larger operations may need integration with quality management, ERP, or supplier-management systems.
At goods receipt, verify more than quantity and appearance. Match the supplier lot, material code, label, and certificate of analysis or conformance where required. For high-risk packaging, retain sample images or physical retention samples according to the company’s quality procedures. These records become valuable when a complaint involves faded codes, weak seals, label lifting, damaged cushioning, or unexplained product exposure.
On the line, controls should focus on the failure modes that matter. A film run may require checks for gauge, winding, seal integrity, and visual defects. A thermal printing operation may need barcode verification after the label has experienced realistic handling. Anti-counterfeit labels should be checked for correct placement, serialization logic, and tamper function. The control plan should say who checks, what acceptable results look like, how often checks occur, and what happens when a result fails.
Change control is the point where compliance is won or lost
Packaging supply chains change constantly: a resin source changes, a coating is reformulated, a ribbon supplier updates its ink system, a printer moves production, or a regulatory requirement evolves. Not every change needs full requalification, but every change needs triage.
A PPCS change-control form should ask whether the modification affects composition, dimensions, performance, contact status, print quality, security features, environmental claims, approved markets, or existing test evidence. It should require a documented risk decision before implementation. Where the impact is material, the review may call for new samples, line trials, updated declarations, revised artwork approval, customer notification, or additional testing.
One frequent mistake is accepting “no change to performance” as sufficient assurance. Performance may remain similar while composition, regulatory status, supplier location, or traceability changes. Conversely, a small artwork amendment can create a major risk if it affects regulatory text, warning symbols, barcode content, or anti-counterfeit identifiers.
A Compact PPCS Internal Audit Trail
An effective internal audit does not need to mimic an external inspection. It should test whether the system can retrieve evidence and whether real operations follow it. Select a finished product, then trace backward through its packaging components. Can the team identify the exact film, label, ribbon, cushioning material, and foil used? Can it show their approved specifications, supplier status, applicable declarations, lot records, and recent change history?
Then reverse the direction. Choose a packaging material currently on the dock or line and trace forward. Which products and markets can receive it? Is the current artwork approved? Is the material within its storage period? Are there any unresolved supplier deviations? This two-way traceability reveals gaps that document reviews alone often miss.
Where Quality and Safety Teams Should Be Most Skeptical
Be cautious with expired declarations that are repeatedly carried forward without supplier confirmation. Question test reports that do not clearly identify the tested construction. Treat recycled-content, recyclability, compostability, and “free from” claims as controlled statements, not sales language. Watch for supplier substitutions at converter level, especially when packaging is purchased through distributors or printers rather than directly from the material producer.
Also avoid the assumption that a packaging component is compliant simply because it was used successfully before. Regulations, destination markets, chemical restrictions, customer requirements, and formulations can all change. Historical use is helpful context; it is not a substitute for current evidence.
Making PPCS Compliance Sustainable Over Time
The strongest PPCS compliance system is one people can actually maintain. Assign owners for specifications, supplier evidence, artwork, environmental claims, and regulatory monitoring. Set review dates based on risk rather than applying the same interval to every item. Train purchasing teams to recognize when a “like-for-like” substitution is not truly like for like. Give production teams clear visual references for approved labels, films, and printed codes.
For organizations navigating lightweight films, water-based adhesives, mono-material structures, nano-scale security coatings, and rapidly changing packaging rules, disciplined documentation is not administrative drag. It is the bridge between material innovation and safe commercial use.
PPCS compliance turns packaging knowledge into a usable chain of custody. When the next audit, customer questionnaire, supplier change, or product incident arrives, the goal is simple: the team should not have to reconstruct the story. The record should already tell it.
Recommended News
 Sep 15, 2026PPCS Compliance Explained: Packaging Data, Documentation, and Audit ControlsPPCS compliance explained: build traceable packaging data, controlled documentation, and audit-ready controls to reduce risk and strengthen market confidence.
 Sep 15, 2026PPWD Compliance: How Packaging Producers Can Prepare for EU Waste RulesPPWD compliance guide for packaging producers: prepare for EU waste rules with smarter materials, recyclability, EPR planning, and practical design steps.
 Sep 15, 2026How to verify a mono material recyclable packaging manufacturerVerify a mono material recyclable packaging manufacturer with practical checks on composition, recyclability evidence, certifications, performance, and factory controls.
 Aug 27, 2026Where to find packaging specification resources for compliance checksPackaging specification resources: discover trusted regulations, test standards, and supplier documents to streamline compliance checks, reduce risk, and approve packaging confidently.
 Aug 22, 2026How to verify whether recyclable flexible packaging in Europe meets PPWR expectationsRecyclable flexible packaging Europe: learn how to verify PPWR readiness, assess sorting and barrier performance, and avoid weak claims with a practical evaluation framework.
 Aug 16, 2026China Enforces Eco-Environment Code, Raising Export Packaging Compliance RequirementsChina enforces its Eco-Environment Code, tightening export packaging compliance for food, FMCG, e-commerce, and pharma. Learn the new risks, certification checks, and sourcing actions now.
 Aug 05, 2026Packaging Compliance in North America: Which Labels and Material Rules Matter Most?Packaging compliance North America explained: learn the label, bilingual, material, recyclability, and EPR rules that matter most to reduce risk and speed market access.
 Jul 14, 2026Packaging Compliance Materials Guide for Plastic Ban ReadinessPackaging compliance materials guide for plastic-ban readiness: compare films, labels, cushioning, and print systems to reduce risk, protect performance, and stay ahead of changing regulations.
 Jul 13, 2026Biodegradable Packaging Compostable: Key Claims, Standards, and Common MistakesBiodegradable Packaging compostable explained: learn the key differences, standards, compliance checks, and common claim mistakes before choosing or marketing sustainable packaging.
 Jul 10, 2026How Mono Material Packaging Affects Recyclability and Shelf AppealMono material packaging can improve recyclability without sacrificing shelf appeal. Discover key trade-offs, hidden risks, and practical evaluation tips for smarter packaging decisions.
 Jul 04, 2026Mono Material Packaging Europe: What Changes Under New Recycling RulesMono material packaging Europe is rapidly becoming a compliance and cost priority. Learn how new EU recycling rules reshape packaging design, market access, and competitive advantage.
 Jul 01, 2026Mono Material Flexible Packaging: When It Works and Where It Falls ShortMono material flexible packaging explained: discover where it improves recyclability and efficiency, where barrier and machinability limits remain, and how to judge the right fit.
 Jun 29, 2026Compostable Sustainable Packaging in 2026: What Regulations and Costs Are ChangingCompostable sustainable packaging in 2026 is being reshaped by stricter regulations and shifting costs. Learn where it fits, what compliance demands, and how to choose smarter, scalable packaging strategies.
 Jun 28, 2026PPWR Packaging Europe: What Changes for Packaging Specs in 2026PPWR packaging Europe in 2026 will reshape packaging specs across films, labels, adhesives, and cushioning. Learn the key compliance shifts, risks, and smart actions brands should take now.
 Jun 25, 2026Mono-Material Recyclable Science Explained for Practical Packaging DesignMono-material recyclable science explained for practical packaging design. Learn how to balance recyclability, barrier performance, compliance, and cost with smarter material choices.
 Jun 24, 2026Packaging Compliance Resources for PPWR and Plastic Ban ReadinessPackaging compliance resources for PPWR and plastic ban readiness: learn how to assess materials, labeling, recyclability, and supplier data to reduce risk and stay market-ready.
 Jun 21, 2026Sustainable Packaging Materials Certification: What Standards Matter in 2026Sustainable packaging materials certification in 2026: learn which standards truly matter for recyclability, compostability, fiber sourcing, and compliance to reduce risk and choose smarter packaging.
 Jun 21, 2026How to Evaluate PLA PBAT Packaging for Cost, Strength, and CompliancePLA PBAT packaging evaluation starts with real cost, strength, and compliance. Learn how to compare suppliers, reduce sourcing risk, and choose packaging that performs.
 Jun 20, 2026Sustainable Packaging Materials Trends Shaping 2026 Compliance PlansSustainable packaging materials are redefining 2026 compliance plans. Explore key trends, risks, and smart material choices that improve recyclability, traceability, and cost control.
 Jun 16, 2026Sustainable Packaging Science and the 2026 Compliance ShiftSustainable packaging science is reshaping 2026 compliance, helping brands balance recyclability, protection, traceability, and cost before new rules tighten.
 Jun 12, 2026How PLA Biodegradable Packaging Performs Under New Plastic Ban RulesPLA biodegradable packaging under new plastic ban rules: explore where it delivers compliance, protection, and cost efficiency—and where smart packaging design still matters.
 Jun 11, 2026Vietnam Requires ISPM15 and REACH Declarations for ImportsVietnam Requires ISPM15 and REACH Declarations for Imports from July 1, 2026. Learn how the new packaging compliance rule may impact customs clearance, costs, and shipment planning.
 Jun 10, 2026EU PPWR Rule Takes Effect July 1: Recyclability Proof Required for BOPP/PET Film ExportsEU PPWR rule takes effect July 1, requiring recyclability proof for BOPP/PET film exports. Learn compliance risks, EN 13432 or ISO 14855 document needs, and how to avoid EU customs delays.
 Jun 06, 2026Green Packaging Becomes an EU Market Entry RuleGreen packaging is becoming a real EU market entry rule. Learn how BOPP Barrier Films, Stretch Wrap Films, and RFID Smart Labels exporters can meet new compliance, certification, and packaging cost requirements.